Продукт
E+H Cerabar PMC71B Digital Pressure Transmitter
PMC71B
The Endress+Hauser Cerabar PMC71B is a high-precision digital pressure transmitter designed for reliable absolute and gauge pressure measurement in liquid, gas, and steam applications. Featuring an oil-free Ceraphire® ceramic process membrane, it delivers exceptional abrasion resistance, chemical compatibility, and complete vacuum stability in demanding industrial environments.
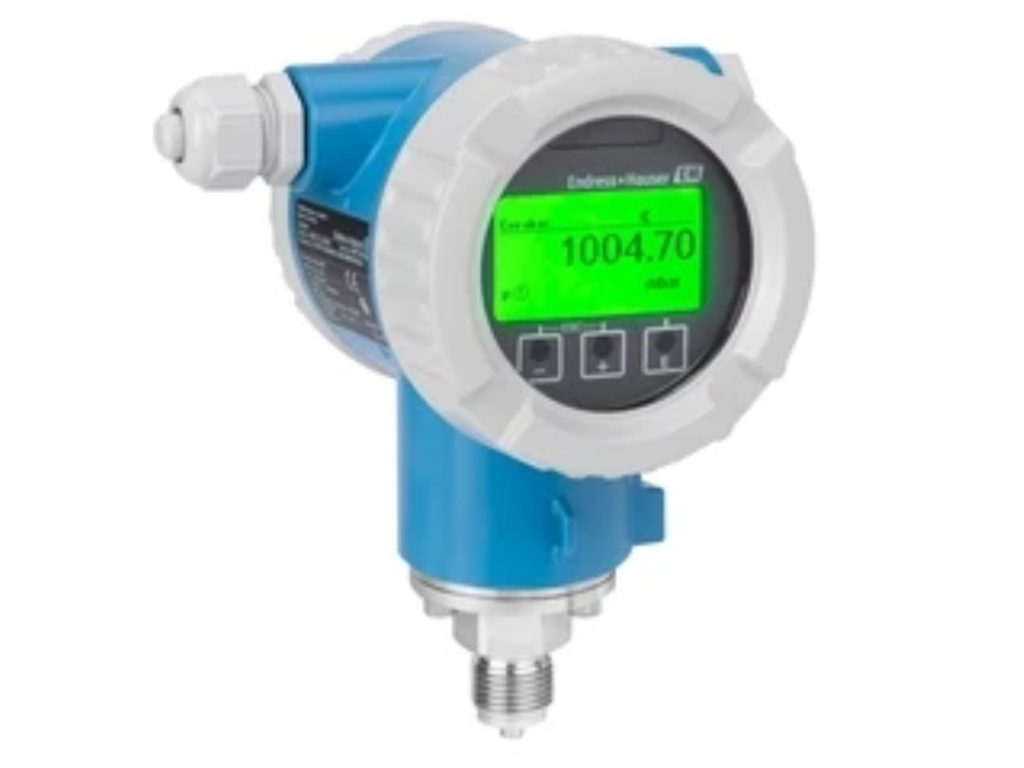
The Endress+Hauser Cerabar PMC71B represents the next generation of smart digital pressure transmitters, engineered to deliver maximum process safety, high measurement accuracy, and long-term stability across diverse industrial applications. Built with an oil-free, high-purity (99.9%) Ceraphire® ceramic process membrane, the PMC71B is purpose-built to withstand aggressive, corrosive, and highly abrasive media where traditional metallic diaphragms are prone to wear or failure.
Designed for demanding operating conditions, the Cerabar PMC71B features integrated ceramic membrane breakage detection, providing an added layer of safety during severe overpressure spikes or deep vacuum operations. The dry ceramic sensor eliminates the risk of fill-fluid contamination, making it ideal for high-vacuum distillation, chemical reactors, and hygienic processes.
Equipped with advanced Heartbeat Technology, the Cerabar PMC71B provides continuous self-diagnostics, device verification, and process monitoring without interrupting ongoing operations. Field operators can perform effortless wireless commissioning, diagnostic checks, and parameter configuration via Bluetooth® connectivity using the SmartBlue app. The transmitter also seamlessly integrates into modern control architectures via 4–20 mA HART, PROFIBUS PA, or PROFINET with Ethernet-APL protocols. Its clear backlit display with intuitive wizards ensures fast setup and error-free operation.
Applications:
-
Chemical & Petrochemical: Pressure and level measurement in aggressive chemical reactors, acid storage vessels, and vacuum distillation units.
-
Oil & Gas Processing: Accurate gauge and absolute pressure monitoring in upstream, midstream, and downstream process lines.
-
Water & Wastewater Treatment: Hydrostatic level measurement and pressure control in sludge tanks, filtration units, and chemical dosing systems.
-
Food & Beverage: Hygienic pressure measurement in tanks, pipelines, and CIP/SIP cleaning processes requiring high abrasion resistance.
-
Power & Energy Generation: Steam drum pressure monitoring, auxiliary boiler control, and cooling water loop measurements.
Technical Specifications:
-
Measuring Principle: Absolute and gauge pressure
-
Process Membrane: Oil-free Ceraphire® ceramic (99.9% Al2O3)
-
Measuring Ranges: 100 mbar to 40 bar (1.5 psi to 600 psi)
-
Reference Accuracy: Standard up to ±0.05%, Platinum up to ±0.025%
-
Turndown Ratio: Up to 100:1
-
Process Temperature Range: -40 °C to +150 °C (-40 °F to +302 °F)
-
Ambient Temperature Range: -40 °C to +85 °C (-40 °F to +185 °F)
-
Max. Overpressure Limit: Up to 60 bar (900 psi)
-
Vacuum Resistance: 0 mbar absolute (fully vacuum resistant up to +150 °C)
-
Output / Communication: 4–20 mA HART, PROFIBUS PA, PROFINET with Ethernet-APL, optional Bluetooth®
-
Housing Material: Die-cast aluminum or 316L stainless steel
-
Certificates & Approvals: ATEX, IECEx, CSA, NEPSI, SIL2/SIL3 functional safety
FAQ
-
Q1: What are the main benefits of the Ceraphire® ceramic membrane in the PMC71B?
A: The oil-free Ceraphire® ceramic membrane offers superior chemical resistance, extreme surface hardness against abrasive media, and full vacuum stability up to +150 °C without the risk of diaphragm fill-fluid leakage.
-
Q2: Can the Cerabar PMC71B be configured remotely?
A: Yes, optional Bluetooth® connectivity enables wireless configuration, diagnostics, and status checks via the SmartBlue App from up to 10 meters away.
-
Q3: What communication protocols are available for this model?
A: The PMC71B supports standard 4–20 mA HART, PROFIBUS PA, and PROFINET with Ethernet-APL for seamless digital plant integration.
-
Q4: How does Heartbeat Technology improve plant safety?
A: Heartbeat Technology conducts real-time self-monitoring and device verification without process interruption, detecting potential issues like impulse line blockage or power fluctuations early.
Документы продукта
Открыть технические документы.
Один раз укажите рабочую почту и WhatsApp для доступа ко всем документам.